Hey everyone, it’s Jake from the TIG Welding Machine supplier team—let’s cut to the chase today because I know a lot of you new welders or even small fab shop owners hit a wall when you first start messing with TIG weld bead width. Like, “why is my bead 2x wider than my buddy’s when we used the same machine?” It’s not luck, it’s just understanding what actually controls that width. And since we sell TIG machines for a living, we deal with this question every single day from guys trying to nail down their first perfect bead. TIG Welding Machine

First off, let’s make sure we’re on the same page here: TIG welding bead width is literally the distance between the two outer edges of the molten weld pool that solidifies, right? Not the width of your filler wire, not the width of your tungsten—actual fused metal from the base material and filler if you’re using it. A lot of new folks mix that up, and that’s where the confusion starts.
Let’s break down the core factors because that’s what matters when you’re working with a TIG welding machine. First up, amperage. Yeah, I know, amperage is heat, so if you crank up the amps, you get more molten metal, which makes a wider bead. Duh, but here’s the catch— it’s not linear. If you go from 100 amps to 200 amps, your bead width doesn’t double. It expands more in the direction of penetration, actually? Wait no, wait—for thin gauge metal, yeah, higher amps = wider bead. For thick stuff, you’re just digging a deeper hole instead of making the sides spread. That’s a key point. Like, if you’re welding 16 gauge aluminum, 80 amps might give you a ¼-inch bead, but bump it to 120 amps and that same thin metal will have a 3/8-inch bead, no question. But if you’re welding ½-inch steel, cranking to 150 amps might widen the bead only by an 1/8-inch because most of that heat is going into melting deep, not spreading outward. That’s something we teach all our customers when they get a TIG machine from us—don’t just crank amps expecting more width without checking your material thickness first.
Next, travel speed. This is the one I see people mess up way more than amperage. If you move too slow, the molten pool has way more time to spread out sideways, so your bead gets wider. If you zip too fast, the pool barely has time to melt the base material, so your bead is skinny and maybe even incomplete. For example, on 18 gauge stainless, a travel speed of 3 inches per minute gives a 5/16-inch bead, but drop that to 1.5 inches per minute and you’re looking at almost a ½-inch bead, plus way more buildup that might cause warping. A lot of new welders think “slower = better penetration” and it does, but not at the cost of bead width getting out of hand. We always tell folks to practice on scrap of their actual material first—set your amperage, then tweak travel speed until your bead is exactly what you need.
Then there’s the angle of your tungsten and filler wire. Let’s get specific: your tungsten tip angle is a huge one. A sharp 15-degree point vs. a dull 45-degree tip. Wait, if your tungsten is sharp, the arc is more concentrated, right? So the molten pool is smaller, so your bead is narrower. A dull tip spreads the arc out, so wider pool, wider bead. That’s a quick fix if you need to widen a bead just a little without cranking amps. Also, your work angle—if you’re leaning too far forward (like, more than 15 degrees from perpendicular), that can push the arc forward and spread the sides, widening the bead. If you’re perpendicular, the arc hits straight down, so the pool stays tighter. And filler wire: if you feed it too far into the molten pool, you’re adding extra molten metal on the sides, which widens the bead. If you feed it right at the leading edge of the pool, you get less filler, so narrower bead. We see this all the time when a shop owner calls us saying their TIG machine is “broken” because their beads are too wide—turns out their welder was shoving filler in too deep, no machine issue at all.
Wait, shielding gas? I almost forgot that. Argon is the standard for TIG, right? If your gas flow is too low, the weld pool gets contaminated, but also the arc is unstable, can spread out a little. If gas flow is too high, you get turbulence, which messes with the arc too. Optimal flow is usually 15-25 CFH for most setups, depending on your gas cup size. If you use a bigger gas cup, that actually encloses the arc more? No, wait—bigger gas cup means more area for shielding, so the arc can spread a little, making a wider bead. A smaller gas cup keeps the arc tight, narrower bead. That’s another tiny adjustment you can make without touching amperage or travel speed.
Now, let’s talk about how this applies to real-world jobs, because we’re TIG machine suppliers, not just textbook writers. For example, if you’re doing a project where you need a narrow, crisp bead—like custom car body panels (18 gauge steel) or small jewelry—you’ll crank lower amps, move faster, use a sharp tungsten, a small gas cup, and feed filler sparingly. If you’re doing something like thick pipe welding (½-inch carbon steel), you need a wider bead to make sure the fusion covers the joint, so you’ll use a bit higher amps, slower travel, maybe a slightly duller tungsten, and a medium gas cup.
But here’s the thing: there’s no “one-size-fits-all” bead width. It depends on what the job needs. We’ve had customers buy a TIG machine from us and say “my beads are always 3/8-inch wide, but I need them ¼-inch” and we just walk them through adjusting travel speed from 2.5 IPM to 4 IPM, that’s it. No need to change settings drastically. That’s why investing in a good TIG machine matters—some cheap machines give you a wonky arc that’s hard to control, so even if you tweak all those factors, your bead width is inconsistent. Our machines have stable amperage control, so when you set 100 amps, it stays 100 amps, no random spikes that widen the bead. That’s a big difference, especially for guys who are doing production work and can’t afford variable bead ruining parts.
Wait, also, filler metal diameter. If you’re using 1/16-inch filler vs. 3/32-inch, obviously the thicker filler adds more metal to the weld pool, so wider bead. That’s another small factor people overlook. Like, if you switch from 1/16 to 3/32 filler without changing anything, your bead will get wider by like 1/8-inch on average.
Let me bust a common myth here: a lot of new welders think that bead width is just about how hard you push the pedal, but it’s way more about control. TIG welding is called TIG (Tungsten Inert Gas) for a reason—you’re controlling the arc, the pool, the filler, all at the same time. I’ve seen a welder with a $500 TIG machine make perfect, consistent ¼-inch beads, and another with a $2,000 machine make messy, inconsistent beads just because they don’t know how to adjust those factors. So it’s not the machine alone, but the machine plus knowing what affects bead width.
And since we’re in the TIG machine supply business, we get questions like “what machine is best for consistent bead width?” The answer is, look for a machine with precise amperage control (least 1 amp increments if you’re doing thin metal), a stable arc, and good gas flow adjustment. Our TIG Welding Machines have both—we designed them for both hobbyists who are just learning, and small fab shops that need consistent results for production.
Now, let’s talk about troubleshooting if your bead width is off. If it’s too wide: slow down travel speed, lower amperage, use a sharper tungsten, smaller gas cup, thinner filler. If it’s too narrow: speed up a little, raise amperage slightly, dull the tungsten a tiny bit, bigger gas cup, thicker filler. That’s a quick cheat sheet we give all our customers when they pick up a machine from us or order online.
Wait, also, material type. Aluminum vs. stainless vs. mild steel—all have different thermal conductivity. Aluminum conducts heat way faster than steel, so you need higher amps to get the same bead width on aluminum vs. steel. That’s why you can’t just use the same amperage for different materials without adjusting. We always tell customers to test on scrap of their actual material first, because that’s where you get the real bead width you need.
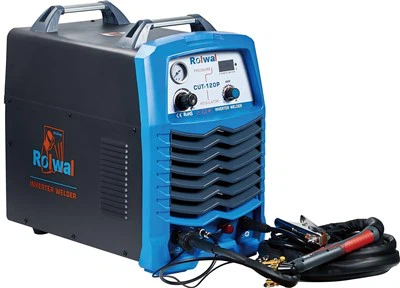
At the end of the day, bead width in TIG welding isn’t some mysterious number only pros know. It’s a combination of controllable factors—amps, travel speed, tungsten angle, gas, filler—that you can tweak once you know what to look for. If you’re struggling with inconsistent bead width or you’re in the market for a reliable TIG welding machine that makes it easier to nail those factors, don’t overcomplicate it. Hit us up to chat through your needs—whether it’s hobby work or production, we’ve got machines that’ll help you get the bead width you want, no guesswork. Just send a message, and we’ll walk you through it.
Self-priming Jet Pump REFERENCES
- "TIG Welding Basics: Control of Bead Geometry" – AWS Welding Handbook, Volume 2, 10th Edition
- "Factors Affecting TIG Weld Bead Dimensions" – Modern Welding Magazine, Vol. 57, No. 3, 2021
- "Practical TIG Welding Techniques for Consistent Bead Width" – Manufacturing Processes Journal, 2022
Lewei Pumps Industry Co., Ltd.
Lewei Pumps Industry Co., Ltd. is one of the most professional tig welding machine manufacturers and suppliers in China, featured by quality products and low price. Please rest assured to buy bulk discount tig welding machine for sale here and get free sample from our factory. Also, customized service is available.
Address: Shanshi Industrial Zone, Daxi Town, Wenling City, Zhejiang Province, China
E-mail: info@rolwal.com
WebSite: https://www.rolwalpumpweld.com/
